China Lost Foam Casting Delivers Precision Manufacturing for Complex Metal Components
2026-10-12
Complex metal components demand more than conventional casting can offer. China’s lost foam casting is changing that—delivering precision, intricate geometries, and near-net shapes with fewer secondary operations. At the center of this shift is Zhaoyuqi, a brand pushing the boundaries of what’s possible in metal manufacturing. Read on to see how this process works and why it’s becoming the go-to choice for complex parts.
Pouring Molten Metal into Foam Patterns: The Core of Lost Foam Casting
The lost foam process hinges on a simple but unforgiving moment: molten metal rushing into a cavity shaped by an evaporating foam pattern. Unlike traditional sand casting, there is no separate core or mold cavity to define the internal geometry. The foam itself becomes the space, and as the liquid metal flows, it vaporizes the pattern almost instantly. This isn't just filling a void—it's a race between heat and material displacement. The metal must push forward fast enough to replace the foam before the foam collapses into a residue that could trap gases or create folds.
Temperature and pour speed matter more here than in most casting methods. Too slow, and the foam melts into a viscous mess that clogs the flow path. Too fast, and turbulence can shred the remaining foam, causing solid particles to mix into the metal. Foundries often use ceramic coatings on the foam to channel the vaporized gases outward through vents, but the real skill lies in reading how the metal front behaves. A smooth, continuous pour keeps the foam decomposing at a controlled rate, allowing the metal to take the exact shape of the original pattern without a single void left behind.
What sets lost foam apart is that the pattern never survives the process—it sacrifices itself completely. That disappearance is what enables complex, undercut, and hollow sections to be cast in one piece without cores or parting lines. But it also means every pour is a one-shot deal. If the metal cools too early or the foam fails to evacuate, the entire casting becomes scrap. This is why the moment of pouring is treated less as a mechanical step and more as a controlled burn, where the foam’s vaporization and the metal’s advance must stay in perfect rhythm.
Complex Internal Cavities Without Cores: A Foundry Advantage in China
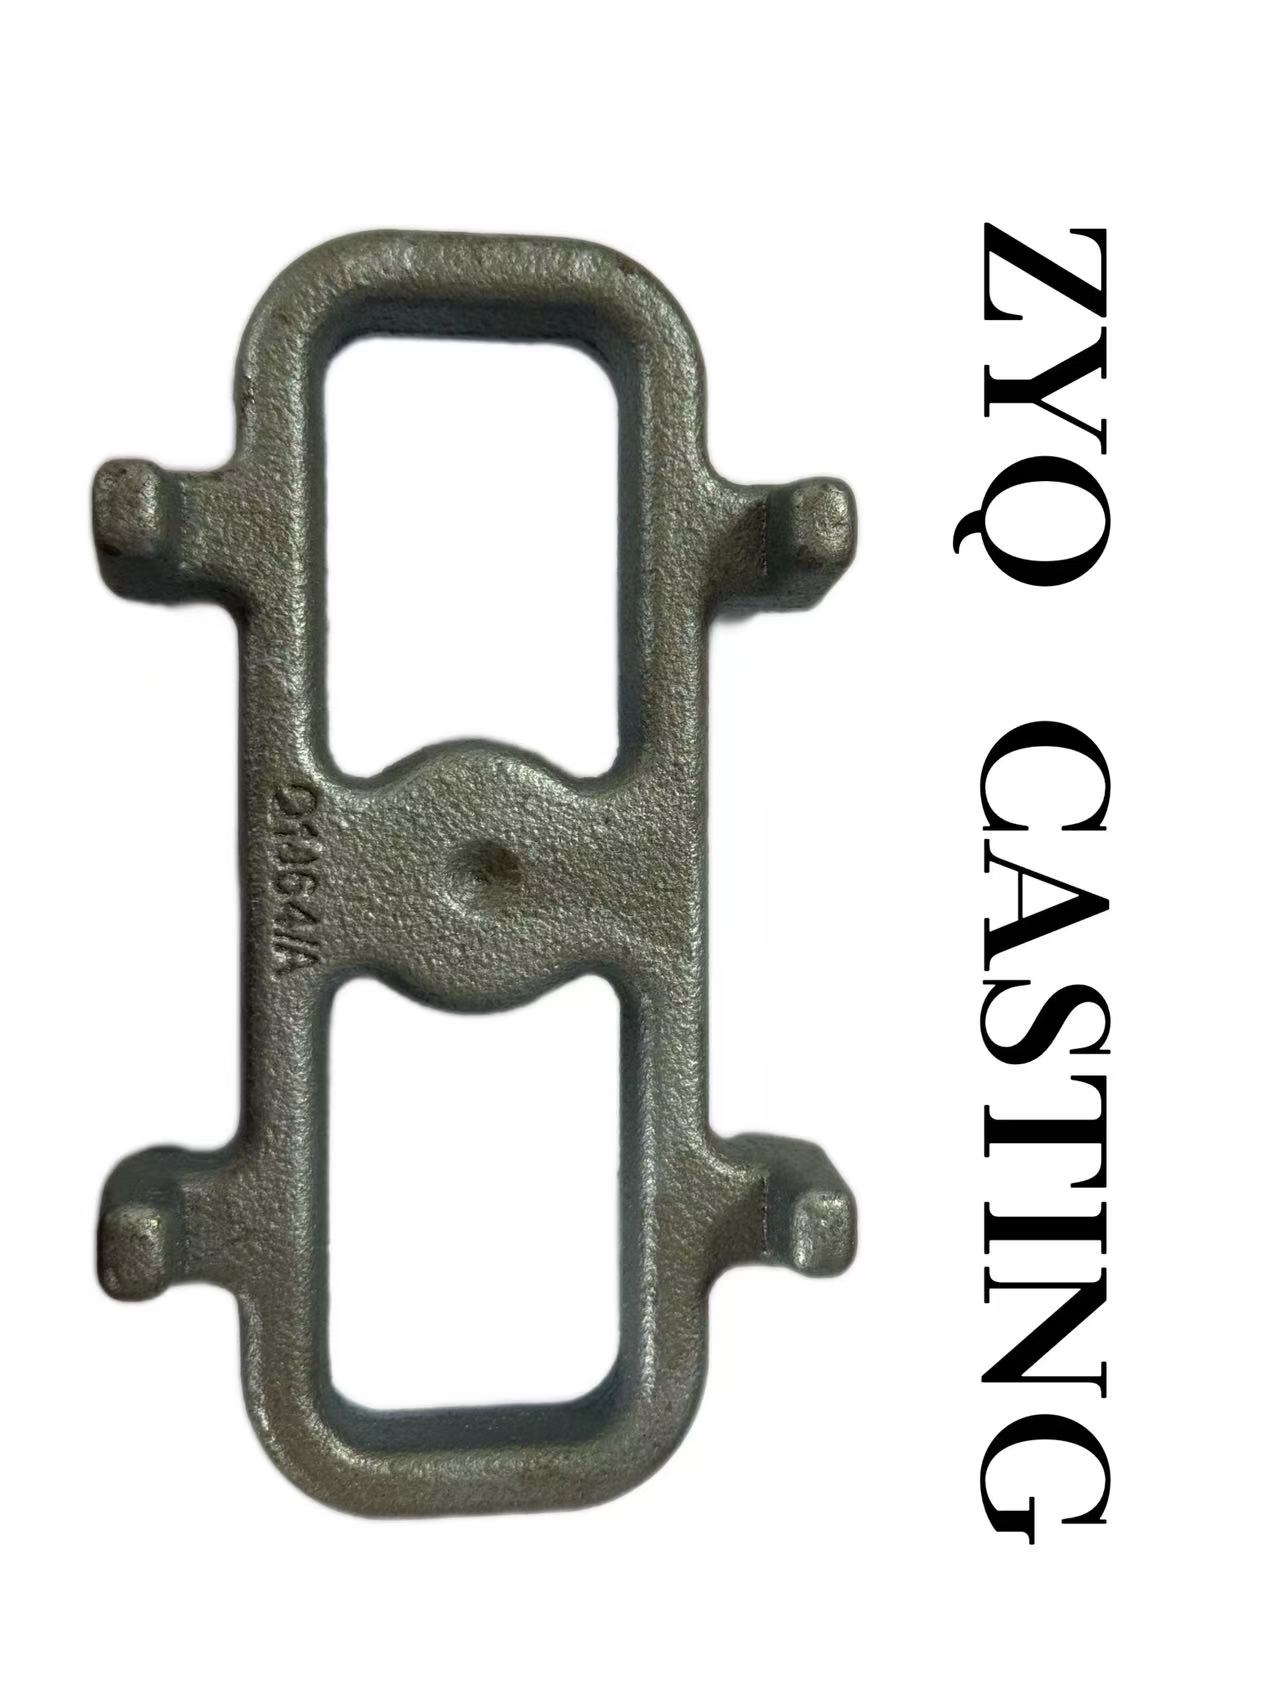
In many foundries, producing parts with intricate internal voids still means assembling multiple sand cores, each with its own parting lines, venting requirements, and fit-up tolerances. Chinese foundries have pushed a different route for selected part families: the cavity is formed directly by a one-piece shell or by a pattern that burns out cleanly, so no separate core is ever placed in the mold. This removes core seams, reduces mismatch between internal passages, and eliminates the need to clean out narrow core prints and vents after casting.
The practical methods vary by alloy and geometry. Investment casting with a soluble or ceramic-lined wax pattern can reproduce curved oil galleries, twisted coolant channels, or valve-body passages without a collapsible core. Lost-foam and full-mold processes go further for large iron and steel housings: the foam pattern already contains the entire internal void network, and the unbound sand simply packs around it. Once the metal displaces the foam, the resulting cavity is already in place, with no core assembly or core-rod support marks left behind.
Chinese suppliers gain an edge here because the cost structure of pattern tooling, slurry dipping, and robotic shell handling is often lower than in high-wage regions, while foundry clusters can iterate quickly on gating and venting to avoid gas defects in blind cavities. For hydraulic manifolds, pump bodies, turbocharger housings, and medical device components, this no-core approach shortens lead time, improves internal surface finish, and lowers scrap rates linked to core shift or core gas. Buyers who qualify such suppliers early can lock in a process advantage that is difficult for core-dependent shops to replicate quickly.
Dimensional Tolerance Levels Chinese Lost Foam Foundries Actually Deliver
A common gap exists between the tolerance figures quoted on paper and what actually arrives on the shipping dock. Many Chinese lost foam foundries will state CT8 or CT9 in initial technical sheets, but after running a few hundred castings, the real dimensional spread often lands closer to CT10–CT12 for ferrous parts, especially once part length passes 500 mm. The drift comes less from the metal pouring itself and more from upstream steps: foam bead fusion variability, coating thickness changes during drying, and slight pattern movement during sand fill and compaction.
Practical measurement data from mid-size carbon steel and ductile iron jobs tells a clearer story. For castings in the 200–400 mm range, a realistic delivered tolerance is about ±0.8 mm to ±1.5 mm on non-critical dimensions, while bores and mating faces may shift an additional 0.3–0.5 mm due to coating buildup. Once dimensions exceed 1,000 mm, local deviations of ±3 mm or more are not unusual, even when the supplier claims a global CT9. Buyers who machine to final size should treat the foundry's claimed band as a starting point, not a guarantee.
Some shops do better, but it shows up in process control rather than marketing language. Look for foam molding rooms with stable temperature and humidity, low-shrinkage refractory coatings, and negative-pressure pouring curves that are adjusted per pattern geometry. The more useful signal is whether the foundry can provide batch dimensional inspection reports for similar parts instead of just a generic tolerance chart. In practice, that capability usually means the difference between a line that drifts and one that holds a usable dimensional window.
Surface Finish Comparisons: Lost Foam vs. Investment Casting for Complex Parts
Surface finish isn't a single number when you compare lost foam and investment casting on complex parts—it varies across thin walls, deep pockets, and internal passages. Investment casting generally produces as-cast Ra values between 1.6 and 3.2 µm, whereas lost foam typically lands in the 6.3 to 12.5 µm range and can climb higher on hidden surfaces. Those extra microns translate into more stock removal, longer blasting cycles, and sometimes a full secondary machining operation.
The gap comes from how each process forms its mold cavity. A wax pattern dipped in fine ceramic slurry creates a dense, smooth shell that reproduces surface details at the micron level. In lost foam, the refractory coating around the foam pattern is coarser and less uniform, especially in deep sections or areas with sharp geometry changes. When the metal vaporizes the foam, gas must escape through that coating, and the resulting turbulence can etch the solidifying surface. Complex parts make this worse because venting paths are longer and coating thickness is harder to control on internal cores.
That doesn't mean lost foam is always the wrong choice. If you're making an intricate manifold or valve body that would require five separate cores in investment casting, lost foam can eliminate core assembly and its associated mismatch defects, but you'll pay for it in surface finish and post-processing. Many foundries will recommend investment casting when the print calls for Ra below 3.2 µm on non-machined surfaces, especially for fatigue-critical parts. If your design can tolerate a rougher finish and you need to cut tooling cost and lead time, lost foam still has a place—just budget for extra vibratory finishing or machining allowance.
Low-Volume to Medium-Volume Runs: Why Lost Foam Beats Traditional Sand Casting
When your production schedule sits between a handful of prototypes and full-scale mass manufacturing, the tooling economics shift dramatically. Traditional sand casting often demands rigid patterns, core boxes, and multiple flasks—even for a few dozen parts. Lost foam eliminates much of that upfront burden. A single foam pattern, easily machined or molded, replaces the entire multi-part sand mold assembly. For runs of 50 to 5,000 units, this means you're not paying for tooling that would only break even at 20,000 pieces.
Beyond cost, complexity drops off the table. Sand casting struggles with undercuts, internal passages, and intricate geometries because each feature usually requires a separate core that must be assembled, seated, and later removed. Lost foam sidesteps this by allowing the foam pattern to include all those details directly. The foam vaporizes during pouring, leaving behind a single, near-net-shape casting without core seams or parting line mismatches. Fewer assembly steps translate into fewer chances for dimensional drift—something that quietly kills profit margins in medium-volume work.
Finally, consider surface finish and post-processing. Traditional sand molds leave a rough texture that often needs extra machining or sandblasting. Lost foam, by comparison, produces a finish closer to investment casting because the foam's smooth surface transfers directly to the metal. For parts that require tight tolerances or cosmetic appeal without secondary operations, that difference alone can justify the switch. You're not just saving on tooling; you're cutting downstream labor and scrap rates that accumulate over hundreds of castings.
Supplier Evaluation Checklist for Precision Lost Foam Casting Projects in China
A practical supplier evaluation for precision lost foam casting in China should begin with evidence, not claims. Request detailed process records from previous projects with comparable wall thickness and weight—coating slurry viscosity logs, foam bead pre-expansion density checks, sand compaction data, and post-pour cooling curves. If the factory cannot share these within a day, their quality control likely depends on individual operators rather than a repeatable system.
During the plant visit, spend most of your time in the pattern molding and coating areas. Look for stable room temperature, clearly marked bead grades, and tooling storage that prevents warping. Also ask how they close the dimensional loop: strong suppliers measure first articles with a CMM or 3D scanner and feed corrections back into the foam tool before volume production. Without this step, you will inherit the cost of iterative sampling.
Commercial checks matter just as much as metallurgical ones. Confirm their experience with your specific alloy family—carbon steel, low-alloy steel, and ductile iron each demand different gating and coating approaches in lost foam. Review export packaging and documentation habits from at least two previous overseas shipments, and clarify who owns pattern maintenance and replacement tooling over the life of the program. A supplier that hesitates on these points is not ready for precision work.
FAQ
It uses expendable foam patterns that remain in the mold, so intricate internal cavities, undercuts, and thin walls can be formed without cores or parting lines, which simplifies tooling and allows near-net shape precision.
Chinese foundries pair lost foam casting with automated sand handling and real-time process control, reducing dimensional variation and porosity in parts used for automotive, hydraulic, and machinery applications.
Because the foam pattern is produced to exact dimensions and replaced by molten metal in a single step, the casting replicates fine details and tight tolerances directly, minimizing post-machining.
Automotive, agricultural machinery, fluid handling, and general industrial equipment benefit from complex manifolds, housings, brackets, and wear parts that need consistent geometry and reduced assembly steps.
It eliminates cores and mold halves, so complex geometries cost less to cast, need fewer machining operations, and show better surface finish and dimensional repeatability.
They use CNC-machined foam molds, controlled coating thickness, precise pouring temperatures, and automated shakeout to keep every batch within specified tolerance.
Yes, the process works with gray iron, ductile iron, steel, aluminum, and copper alloys, letting Chinese foundries serve diverse applications with one flexible method.
Look for in-house pattern making, documented process controls, material certification, and experience with similar component complexity to ensure reliable dimensional accuracy and metallurgical quality.
Conclusion
Lost foam casting in China has matured into a practical choice for complex metal parts where traditional methods struggle. The process starts by embedding a foam pattern in sand and pouring molten metal directly onto it; the foam vaporizes instantly, leaving a near-net-shape component. That simple sequence opens up real design freedom—internal passages, undercuts, and hollow sections can be formed without separate cores, which cuts assembly steps and avoids misalignment issues. Experienced Chinese foundries routinely hold dimensional tolerances tighter than many buyers expect, often within ±0.3 mm depending on part size, and the as-cast surface typically falls between sand casting and investment casting. For parts with intricate internal geometry, lost foam often delivers a smoother finish than sand casting and avoids the parting-line flash common in other methods, though investment casting still wins for very fine external detail.
The process really earns its place in low-to-medium production volumes. Unlike traditional sand casting, lost foam does not require pattern draft, core prints, or mold halves, so design changes are cheaper and faster to implement—making it a strong fit for prototyping through a few thousand pieces per year. When sourcing from China, a practical evaluation checklist should cover more than price: look for documented tolerance capability on similar geometries, sample reports with surface roughness data, foam pattern quality control, and experience with your alloy family. Ask how the foundry handles thin walls, internal channels, and post-casting cleaning. The best suppliers will explain their limitations honestly rather than promising impossible precision, and that transparency is usually a better sign than glossy marketing claims.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/