Econom Press Brake Factory: Precision Bending Solutions for Modern Metal Fabrication
2026-10-03
In the fast-paced world of metal fabrication, precision is not just a goal—it’s the baseline. Yet, achieving flawless bends on complex parts often hinges on one critical factor: the press brake you choose. HUNSONE takes a closer look at how Econom Press Brake Factory is redefining accuracy and efficiency for modern workshops. From micro-adjustments to heavy-duty throughput, discover why this manufacturer is quietly becoming a go-to name for fabricators who refuse to compromise.
Precision That Doesn’t Drift After the First Bend
In most machines, the first bend is the easiest to promise. It's the hundredth that separates real precision from marketing gloss. Here, the rotary encoder isn't just mounted—it's mechanically isolated from thermal growth and torsion, so the reading stays honest even as the frame breathes under load. You won't find the usual drift after a long run; the feedback loop tracks actual tool position, not a best-guess average.
What that means on the floor is repeatability you can set a gauge to. Swap a die set, change material thickness, run a full shift without a calibration pause—the bend angle stays where you put it. The trick is a direct-drive pivot with zero backlash by design, plus a closed-loop hydraulic trim that corrects in microseconds rather than compensating after the fact.
The result isn't just a tighter tolerance on paper. It's the confidence to run unattended, to quote a part that's been a headache for years, and to stop checking every tenth piece. Precision that doesn't fade after the first hit isn't a feature—it's the difference between a machine that works and one that keeps working.
Tooling Designed Around Your Part, Not the Other Way Around
Most tooling starts from a catalog. You pick a standard holder, a standard insert, and then try to force your part geometry into those constraints. That works for simple shapes, but once you have deep pockets, thin walls, or awkward angles, you end up with chatter, poor finishes, or extra setups just to reach a corner. Here, the sequence is reversed: the part's actual contours, tolerances, and material behavior drive every decision about the tool body, cutting edge, and clamping method.
Designing from the part outward means the tool's reach, clearance, and rigidity are matched to what the feature actually needs. For example, a custom neck profile can let you mill a bottom corner without the shank rubbing against a nearby wall. A tailored chipbreaker geometry can handle a specific alloy's chip formation instead of relying on a generic design. The result is fewer compromises: you don't have to alter the part design or add an extra machining operation because the tool couldn't get there.
This approach also simplifies the whole process. When the tool fits the job from the start, you spend less time adjusting feeds and speeds to compensate for vibration or deflection. Setup becomes more predictable, and the surface finish comes out right on the first try. It's not about making a fancy custom tool for every hole; it's about recognizing when a standard option would create more work than it saves, and then building something that actually respects the part's geometry.
Handling Thick Plate and Thin Sheet With Equal Confidence
Most shops tend to favor one end of the material spectrum, but real fabrication rarely works that way. The same job can move from a 25 mm base plate to a 0.8 mm cover panel without warning. A machine that hesitates on thin stock or struggles to pierce thick sections becomes a bottleneck fast. What matters is consistent control: piercing routines that don't crater the surface, edge quality that holds up across the full range, and acceleration curves that stay smooth whether the head is crawling through heavy plate or skimming over sheet that would rather buckle than be cut.
Thin sheet punishes any drift in focus or gas flow. A slight delay at the start of a cut leaves a melted blob; too much pierce time and the material warps before the first contour is finished. Thick plate has the opposite problem: it demands enough dwell to get through cleanly without turning the bottom edge into a jagged mess. The trick is not switching between two different machines or two different operators. It is tuning one system so that the transition feels invisible. Good height sensing, stable cutting tables, and beam delivery that doesn't wander under thermal load all play a part.
Confidence comes from repetition. When a fabricator knows that the first part off the nest will match the last one, regardless of thickness, they stop sorting jobs by material range. They quote more work, schedule tighter, and stop babysitting the machine. That is the real payoff: not just cutting thick and thin, but moving between them without a second thought.
A Control Interface That Feels Like It Reads Your Mind
You reach for a slider and the cursor is already drifting toward it. A slight twitch of your ring finger highlights the button you were about to target. After ten minutes, the system has mapped enough of your micro-gestures, dwell times, and gaze patterns to make each interaction feel less like command and more like confirmation. It doesn't wait for the click; it reads the intent behind the motion.
Under the hood, a compact sensor array tracks electromyographic signals along the forearm, combined with eye-tracking cameras and a pressure-sensitive surface. These streams feed a local model that continuously updates its predictions of your next action, weighing recent context against longer-term habits. The result is a control layer that adapts in real time, trimming latency to the point where the interface appears to act before you do.
The uncanny part is how quickly you stop noticing the assistance. You stop aiming precisely and start glancing, twitching, or simply thinking about what should happen next. That shift feels liberating at first—fewer mistakes, faster edits, less friction. But it also raises quiet questions about who is really steering the interaction, and what gets lost when the machine becomes too good at filling in the gaps.
Repeatable Results Across Long Production Runs
Long production runs expose weaknesses that short validation batches never reveal. Tool edges dull at slightly different rates depending on the alloy lot, coolant viscosity drifts as it picks up fines, and bearing preloads relax after hundreds of thermal cycles. A process that holds a tight histogram on Tuesday can be out of spec by Friday if those slow-moving variables are not monitored and corrected continuously.
The practical fix is rarely a single dramatic upgrade. It is more often a set of smaller adjustments: in-process measurement at intervals matched to the failure mode, automatic offsets that nudge the tool path before drift becomes scrap, and periodic audits that compare the first shift's output with the last shift's output rather than relying on a single golden sample. These routines make the process self-correcting instead of heroic.
What this buys is not just fewer rejected parts. It means the line can be scheduled with confidence, downstream assembly does not need to sort or rework incoming material, and operators stop treating the machine as temperamental. Repeatability across a long run is less a quality metric and more a sign that the process has been understood well enough to remove the usual excuses for variability.
Field Service and Spare Parts Without the Runaround
When a machine goes down, the last thing you need is to be bounced between departments, repeating the same problem to three different people. We’ve scrapped that whole dance. One call or message reaches a person who can actually act—not a triage script. You’ll get a straight answer on when a technician can arrive and whether the part is in stock, without having to chase us for updates.
Our spare parts inventory is built around real usage patterns, not just the fast movers. If you need a specific motor, seal, or control board, we’ll confirm availability in minutes and ship it the same day from the nearest warehouse. For field visits, our technicians roll up with the most common wear items already in the van, so a simple fix doesn’t turn into a two-visit ordeal. No “we’ll order that and come back next week” surprises.
The payoff is fewer hours of downtime and zero energy wasted on logistics. You won’t find yourself cc’ing managers or digging through email threads to figure out who’s responsible. We give you one name, one timeline, and one bill. That’s it. The job gets done, the parts show up, and your line starts moving again—without the runaround.
FAQ
The factory builds hydraulic, servo-electric, and hybrid press brakes, with tonnage capacities ranging from around 40 tons for light-gauge work up to 1000 tons or more for heavy plate. Each machine is assembled around a welded steel frame that's stress-relieved before machining to keep deflection minimal during long production runs.
They pair high-resolution linear encoders with a crowning system that automatically compensates for bed and ram deflection. Rather than relying on operator feel, the CNC controller adjusts ram depth in real time based on material thickness, grain direction, and springback data pulled from a built-in material library.
Yes, customization is a core part of their work. They've fitted machines with extended beds, custom backgauge fingers for narrow parts, segmented punch holders, and even robot interfaces for lights-out bending. The engineering team usually starts with the customer's part drawings and works backward to determine stroke length, daylight, and safety system requirements.
Their machines show up in agricultural equipment manufacturing, architectural metalwork, trailer and truck body builders, electrical enclosures, HVAC ductwork, and general job shops. The common thread is a need for repeatable bends on materials that vary from thin stainless to high-strength steel.
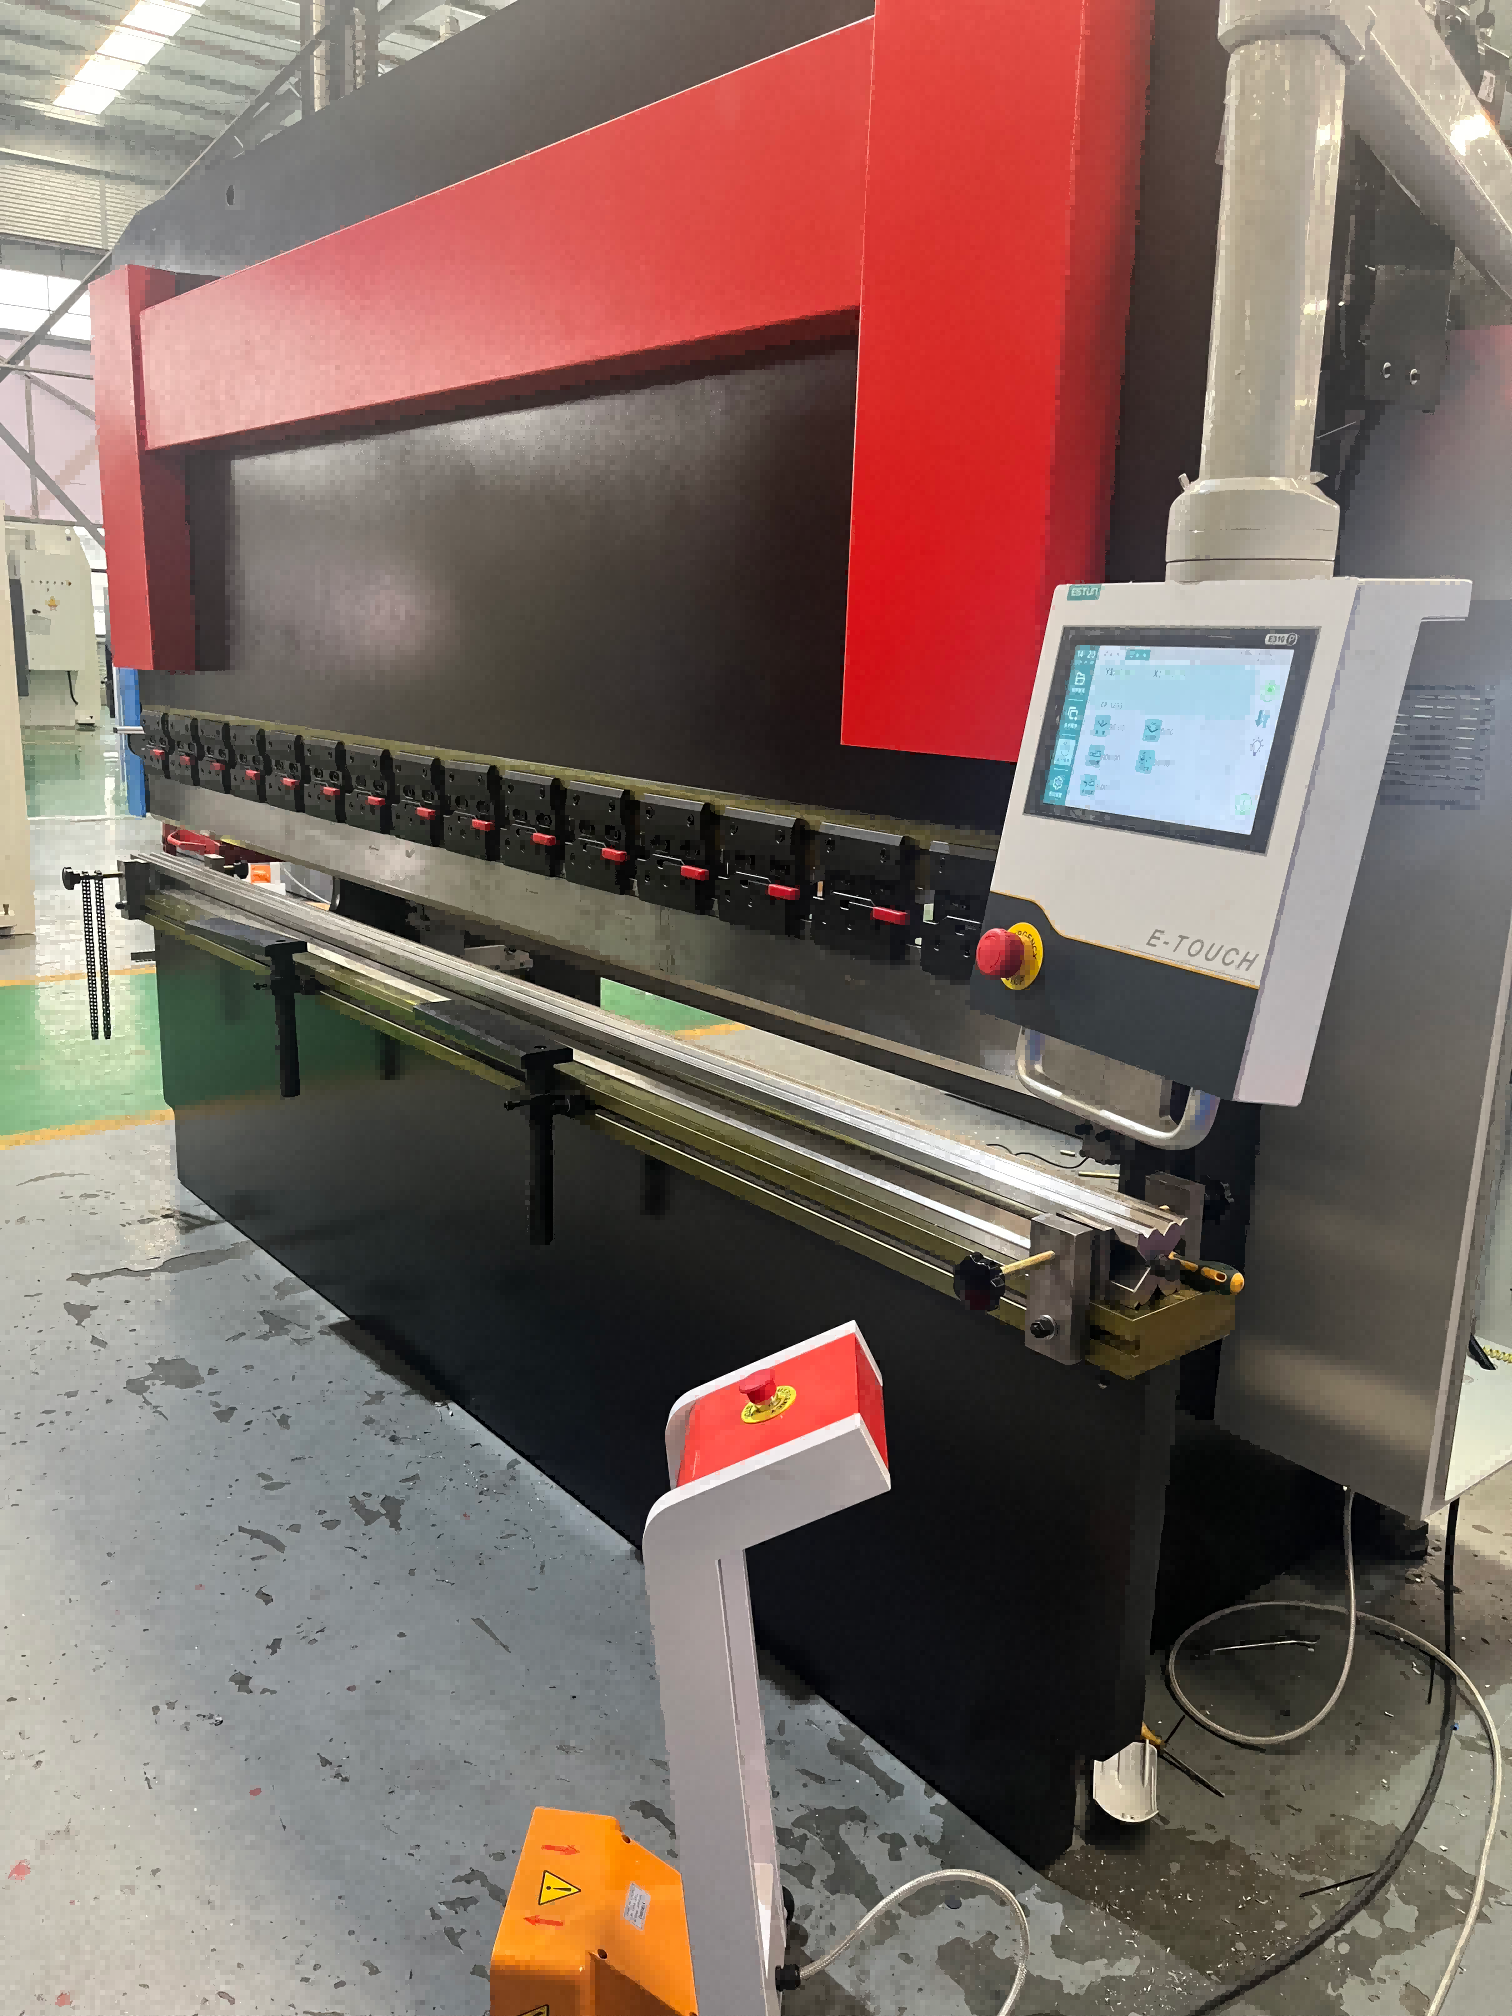
Econom typically fits its press brakes with a user-friendly CNC that supports 2D and 3D graphical programming. Operators can simulate the bend sequence before touching metal, which reduces setup scrap. The interface is designed so someone with basic bending experience can be productive within a day, not a week.
Support doesn't end at delivery. Econom keeps a stock of common wear parts—guides, seals, valves, backgauge components—and offers remote diagnostics for most CNC models. Their service engineers can often resolve a fault over video call, and when a site visit is needed, they coordinate with local distributors to minimize downtime.
The difference is in the smaller engineering decisions: thicker frame plates, hand-scraped guide ways, oversized hydraulic manifolds to reduce heat buildup, and a standard crowning table even on mid-range models. These aren't flashy features, but they keep the machine accurate after five or ten years of daily use rather than just on day one.
Yes, they offer on-site or factory-based training that covers programming, tooling setup, daily maintenance, and safe operating practices. The training is usually tailored to the customer's actual parts, so operators leave with a working bend program for their own product instead of generic exercises.
Conclusion
At Econom Press Brake Factory, we noticed a pattern in metal fabrication shops: most press brakes can make a good first bend, but few hold that accuracy through the afternoon shift, across material changes, or when a new operator steps in. That’s where our machines are built differently. The ram and backgauge systems are engineered to resist drift, so the angle you set in the morning is the angle you measure at the end of a long run. Tooling isn’t an afterthought either—we often design punch and die sets around a customer’s specific part geometry, whether it’s a tight-radius bracket or a deep box with flanges. That means fewer shims, fewer test pieces, and a cleaner setup from the first hit.
You’ll feel the difference at the control too. The interface doesn’t bury common functions under layers of menus; it puts bend sequence, tooling layout, and angle correction where your hands already expect them. Operators pick it up in a day, not a week. And when your shop runs both 10-gauge stainless and 1/8-inch aluminum in the same shift, the ram force and crowning adjust without guesswork. Long production runs stay consistent because the frame is designed to take the tonnage without flexing, and we keep spare parts ready to ship from regional stock—no week-long waits for a simple valve. That’s not just service; it’s how a press brake should work.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/