Econom Press Brake Vendor Delivers Precision Bending Machines for Metal Shops
2026-10-03
Metal shops often assume precision bending machines come with a premium price tag. HUNSONE proves that assumption wrong. As an economy press brake vendor focused on real-world metal fabrication, HUNSONE delivers machines that hold tight tolerances shift after shift. If you’re looking to upgrade your shop’s bending capability without draining your budget, keep reading.
Bending to the Same Angle Every Time, Not Just the First Time
Achieving the correct bend angle on a prototype is one thing; holding that same angle across a full production run is where the real difficulty lives. Material springback varies from sheet to sheet, tooling warms up and shifts dimensions, and hydraulic systems can drift slightly over hours of continuous cycling. If you only validate the first part, you are essentially trusting all the later variation to luck.
What separates a dependable bending process from a constant adjustment battle is feedback that acts on every stroke. Angle measurement systems mounted near the die or load sensors that detect force curves can correct for springback in real time, making tiny compensations before the next bend. This means part number five hundred sees the same angle as part number one—not because the machine was set once, but because it is actively watching each cycle.
Operators sometimes mistake repeatability for rigidity: they want a heavier machine or tighter tooling, but those alone cannot account for material inconsistency. True repeat bending comes from closing the loop between what the machine intended to do and what actually happened at the bend line. That is the difference between a first-article success and a whole shift of parts that fit without hand rework.
The Frame Design Behind Econom's Long-Term Accuracy
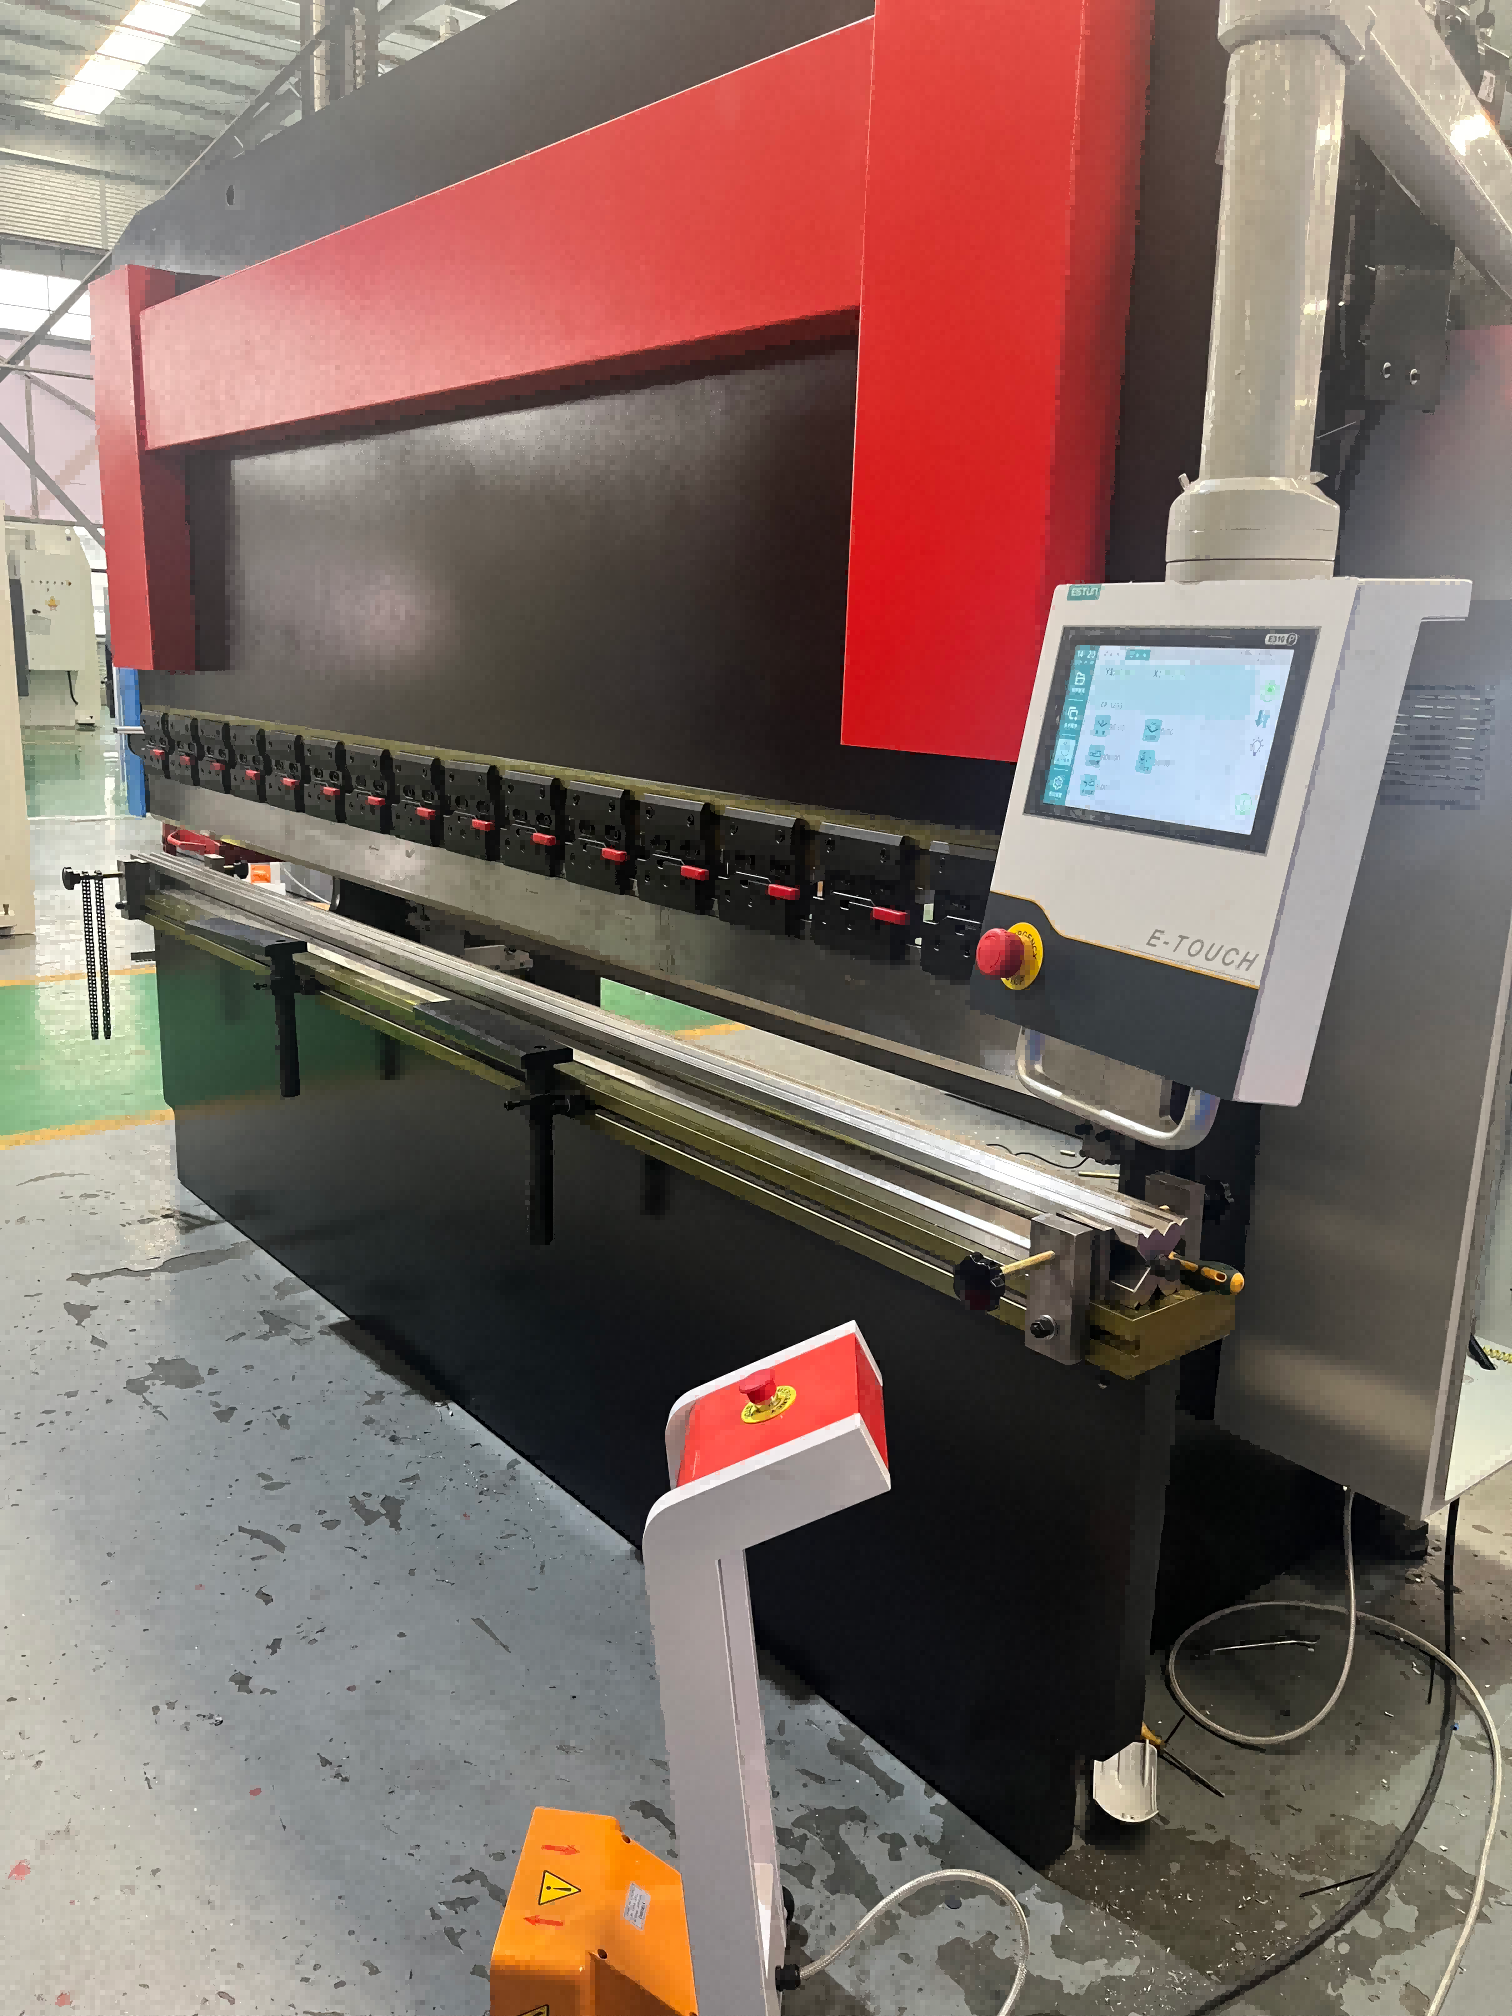
Econom's frame isn't a shell that happens to hold parts in place. The uprights and cross-members are machined as one kinematic loop, so every measurement axis shares a common reference plane. That sounds simple, but it eliminates the slight differential expansion that usually shows up as drift after a few hundred thermal cycles.
The joints are preloaded rather than welded or glued. Welds relax over time; adhesives creep under constant load. Econom uses interference fits and controlled torque on tapered pins, which gives the frame a predictable elastic behavior year after year. The material itself is a stress-relieved aluminum-silicon alloy chosen for its low internal damping and stable modulus across the operating temperature range.
Most long-term error in instruments comes from the frame slowly twisting as residual casting stress works its way out. Econom's frames are rough-machined, thermally cycled, then finish-machined to final tolerance. That extra step removes the microscopic stresses that would otherwise bend the structure imperceptibly over months. The result is a frame that holds its geometry without needing frequent recalibration.
Controls That Don't Require a Degree to Figure Out
The best controls are the ones you never have to think about. A volume knob that clicks with just enough resistance, a light switch that sits exactly where your hand expects it, a temperature dial marked with simple blue-to-red shading—these small choices make everyday tools feel effortless. You shouldn't need a manual, a tutorial, or a YouTube walkthrough just to turn on the heater.
Too many gadgets bury basic functions behind touchscreens and nested menus, forcing you to memorize gestures that make no sense outside a design studio. But the truly clever ones keep it physical and predictable: push to start, twist to adjust, slide to open. If a control requires more than a glance to understand, it's probably overdesigned, not advanced.
Switching Between Jobs Without Losing Your Place
The frustration of clicking into a job posting, reading a few lines, then hitting back only to find yourself at the top of a long list again is all too familiar. A good job board should remember exactly where you left off. When you return to the list, your scroll position stays put, so you can pick up from the next opening without hunting for it.
This might sound like a small convenience, but it changes how you browse. Instead of opening tabs for every role or relying on memory, you can move through listings in a natural flow. Go forward to explore a position, step back when it isn't a match, and land right where you expected. That uninterrupted rhythm keeps your search focused and less mentally tiring.
The same principle applies to filters and search queries. If you've narrowed results by location, salary, or remote options, toggling back from a job description shouldn't erase those choices. Your place includes both the list and the conditions that built it. When those stay intact, switching between jobs feels seamless, not like starting over.
Mixed Material Bending Without a Scrap Pile
Bending mixed materials usually means juggling leftover drops, offcuts, and the inevitable tangle of half-used stock that accumulates around the brake. But it doesn't have to be that way. The real trick is to treat every piece as part of a continuous flow rather than a series of isolated jobs. When you stop thinking about scrap as something that just happens, you start seeing the cuts and bends as a single sequence where one part's remnant becomes the next part's blank. That shift in mindset eliminates the pile before it even forms.
A practical approach starts with nesting at the bending stage, not just at the cutting table. Instead of cutting each blank to exact length and then bending in whatever order the work orders dictate, group parts by material thickness and bend radius. Then sequence them so that the leftover from a long flange naturally feeds a shorter part. It's surprising how often a so-called scrap piece is only scrap because nobody looked ahead. By pairing parts that share a common width, you can run them back-to-back on the press brake, using the same backgauge setup and the same tooling, and the offcut from one part becomes the starting point for the next.
Another layer is to rethink the cut list itself. Many shops default to cutting each part to its final developed length, which creates a constant stream of odd-sized remnants. Instead, cut longer bars or strips and bend multiple parts from a single stick, indexing along its length. This works especially well for brackets, clips, and small flanges that repeat. You bend one, slide the stock forward, bend the next, and only cut them apart at the end. The result is a clean workstation, less handling, and no bin of twisted leftovers waiting to be sorted. It takes a little more planning up front, but the payoff is a bend operation that stays lean without a scrap pile in sight.
A Vendor That Sticks Around After Delivery
Most vendors treat the handoff like a finish line. Sign the acceptance form, watch them pack up, and suddenly every question you have lands in a ticket queue that never moves. A vendor that sticks around after delivery breaks that pattern. They call two weeks later to ask how the team is actually using the tool, not just whether it installed correctly. They notice when a feature is being ignored and suggest a different workflow instead of pushing another paid add-on.
The difference shows up in small, unglamorous ways. You send an email about a weird error message on a Tuesday afternoon and get a reply from the same engineer who built the integration, not a rotating cast of support agents. They update the documentation when you point out a gap. They sit in on a monthly review call without being asked, and they remember the names of the people on your ops team. That kind of continuity is rare because it costs time and doesn't scale well, which is exactly why it's worth looking for.
Before you sign with a vendor, ask for references from projects that went live at least six months ago. Then ask those references when they last heard from the vendor proactively. The answer tells you more than any demo. A vendor who checks in after delivery is treating the relationship as an ongoing responsibility, not a one-time sale.
FAQ
They pair a rigid frame with a fast hydraulic system and a control that holds angle correction automatically, so operators can run 0.030-inch stainless and keep variance under half a degree without constant test pieces.
Econom sends a technician for on-site setup and runs the crew through real jobs during the first week, then keeps phone and remote desktop support open for as long as the shop owns the machine.
The frames are stress-relieved and machined after welding, and the crowning system adjusts along the bed, so even 80,000 PSI material bends stay consistent across a full 10-foot part.
With the closed-loop hydraulics and linear encoders, most shops see bend angle repeatability within ±0.2 degrees and backgauge positioning within ±0.0004 inch after the first warm-up cycle.
The control supports offline programming with automatic bend sequence calculation, and the backgauge has up to six axes, so a job with hemming and offset bends can run from one setup without flipping the part by hand.
Yes, the upper clamp is hydraulic and the lower tooling sits in a quick-change rail, so swapping from a 30-degree punch to a gooseneck takes under five minutes once the crew is familiar with it.
Daily checks are mainly hydraulic oil level, guide rail lubrication, and backgauge screw cleaning; Econom recommends a full fluid and filter change every 2,000 operating hours, and the sealed bearings don't need frequent attention.
The machines come with a laser guard that stops the beam if anything crosses the light path just above the material, and the mute point is adjustable so it doesn't interrupt fast forming cycles.
Conclusion
Econom's press brakes earn their keep in metal shops because they bend to the same angle every single cycle, not just the first one. That kind of repeatability comes from a frame design that resists flex and drift over years of daily use. Shops don't have to retune or compensate after a few hundred parts; the machine holds its settings, so the last piece matches the first. This is a huge deal when you're running a batch of brackets or enclosures and every angle has to fit the next operation. Operators spend less time measuring and more time moving material, which is exactly what a precision bending machine should deliver.
The controls are built for people who already know how to bend metal, not for someone with an engineering degree. Loading a job means the previous setup, tool positions, and bend sequences are right there, so switching between parts doesn't mean starting from scratch. Even when the material mix changes, from thin stainless to thick aluminum, the machine adjusts without leaving a pile of scrap on the floor. And after the install, Econom doesn't disappear. Their support actually sticks around, which matters when a tricky job or a new operator shows up. That kind of vendor reliability is rare, and it's the difference between a machine that sits in the corner and one that becomes the backbone of the shop.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/