High Tenacity Nylon 6 Filament Yarn Supplier Checklist for Quality and Performance
2026-08-30
Sourcing high tenacity nylon 6 filament yarn that actually holds up under load isn’t as simple as comparing spec sheets. Too often, buyers discover hidden weaknesses only after production starts. This checklist cuts through the noise—and explains why teams looking for consistency keep Changshu Polyester on their short list.
Polymer Batch Traceability: Ask for Lot-Level Proof, Not Promises
When a polymer shipment arrives, the physical material in the box rarely matches the brochure. Lot-to-lot variation in melt flow, additive dispersion, or moisture content can shift how a part fills, welds, or ages. That’s why verbal guarantees and generic compliance letters are close to worthless. You need the actual batch data tied to the exact resin lot you’re about to run. Without that, every processing adjustment becomes a guess.
Ask suppliers to link each container or pallet to a specific production run at the resin plant. The proof should include the date of manufacture, quality control test results for critical properties, and any regrind or recycle content in that lot. If a supplier can’t produce lot-level certificates before shipment, treat it as a red flag—not a minor paperwork delay. Certificates that only state “material meets specification” without numeric values are promises wearing a lab-coat costume.
Build traceability into your own receiving workflow. Scan incoming lot codes into your ERP or MES, store the supplier’s batch certificate alongside your internal incoming inspection data, and block material until the lot is verified against your approved list. When a downstream defect appears, you should be able to trace the failed part back to the exact resin lot within minutes—not days of emailing suppliers. That kind of proof is what separates a resilient polymer process from one that hopes for the best.
Why Tenacity Claims Need an Independent Test Protocol
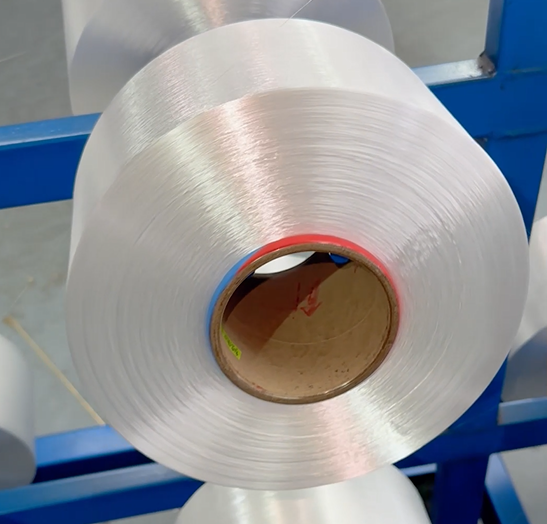
Most manufacturers love to talk about how tough their products are, but those claims usually come from in-house labs with every incentive to cherry-pick favorable results. A nylon fabric might survive 10,000 abrasion cycles when tested on a smooth, flat surface at room temperature, yet fall apart after a few weeks of real-world use on rough concrete in freezing conditions. Without an outside party verifying the test setup, the numbers mean almost nothing to a buyer trying to compare two competing materials.
An independent test protocol removes the obvious conflict of interest by fixing the methodology, the equipment calibration, and the pass/fail thresholds before any sample is evaluated. It forces every product to run through the same gauntlet, whether the manufacturer likes the outcome or not. That kind of standardization turns a vague marketing word like "tenacity" into a repeatable measurement, something an engineer or procurement manager can actually rely on when specifying materials for a demanding application.
The absence of independent verification also lets inferior products hide behind inflated data, which eventually erodes trust across an entire industry. Buyers who get burned once will discount every future durability claim, even from honest suppliers. A credible third-party protocol not only protects the end user from costly failures but also pushes manufacturers to improve their products instead of just polishing their brochures.
Elongation and Shrinkage: The Specs That Surface After Winding
Once a yarn or wire comes off the winder, its length rarely matches the figure recorded under tension. The difference shows up as two numbers that matter more in practice than on paper: elongation and shrinkage. Elongation tells you how much the material can stretch before it breaks or yields, while shrinkage captures how much it gives back once the tension is released and the structure relaxes. These values are not fixed—they shift with winding speed, package hardness, and even the humidity in the room.
What makes post-winding specs tricky is that the winding process itself can mask or exaggerate both. Tight winding builds in residual stress that later releases as shrinkage, especially in elastomeric or high-twist yarns. A loosely wound package may underreport elongation because the fibers have already settled into a more relaxed state. Measuring after a set rest period—often 24 to 48 hours—gives a truer picture, but only if you control temperature and moisture. Otherwise the numbers drift and you end up chasing a spec that never really stabilizes.
Spooling, Packaging, and the Contamination Risks You Can Miss
Many operators treat a fresh spool as clean, but the winding stage is where trouble begins. Extruded filament passes over guides, tensioners, and sometimes bare metal rollers before it ever reaches the spool. Dust, oil mist, and even the faint residue from extrusion lubricants settle on the warm surface and get pressed into the plastic as it cools under tension. Those particles won't wash off and often end up as tiny nozzle clogs or weak spots in printed layers.
Packaging adds another layer of hidden risk. Vacuum-sealed bags with desiccant slow moisture uptake, yet they don't guarantee a pristine product. The bag film itself can shed micro-particles, and repeated handling during shipping causes the filament to rub against the spool flanges, generating fine plastic dust. Once the seal is broken, static charge pulls in airborne lint from the room, which then rides into the hotend. A spool that looks spotless may already carry enough contamination to affect print consistency.
The risks you miss usually come from your own workflow. Touching filament with bare hands transfers skin oils and salts that carbonize at nozzle temperatures. Leaving a partially used spool on a shelf without a cover lets dust settle in the gaps between windings. Even the spool's edge can scrape off micro-filaments if it has a sharp seam. Wiping the first few meters with a dry microfiber cloth before loading and storing open spools in sealed containers with fresh desiccant are cheap habits that prevent most of these failures.
Reading Production Logs for Run-to-Run Consistency Signals
Most run-to-run checks stop at mean and standard deviation, but the real signal sits in the log file's marginal notes: a two-degree temperature swing during the third step, a five-second delay in clamp release, or a pressure overshoot that repeats every six lots. Those small, repeatable deviations don't fail any spec, yet they mark the beginning of tool drift long before the control chart moves.
It helps to read the logs backward from the point of variation. Instead of asking whether a run passed, ask what changed since the last stable batch. Compare gas flow settling times, RF match tuning positions, and quartz part temperatures run over run. When the same nonconformity shows up in three consecutive logs without an alarm, you're looking at a signature, not noise.
That signature is what run-to-run consistency actually measures. A line stays stable not because nothing shifts, but because someone catches the first quiet drift and corrects it while it's still cheap.
What a Supplier’s Documentation Reveals About Its Real Process Control
A supplier's documents often say more through their imperfections than through their polished sections. Look at the revision history on a control plan or work instruction. If you see frequent, dated changes with brief but specific reasons—such as "adjusted torque setting after shaft wear found at line 3"—that signals a living system where operators and engineers actually use the paperwork. A pristine, revision-A-only binder usually means the documents were created for the audit, not for the floor.
The reaction plan column is another tell. Vague entries like "adjust process" or "notify supervisor" suggest the supplier has never really thought through a failure. In contrast, a detailed response such as "stop line, quarantine all parts since last good check, verify fixture clamp pressure, and record deviation in NCR log" shows that someone has walked through an actual problem and encoded the lesson. The specificity of containment, sorting, and restart criteria is where real process control lives.
Raw data sheets and checklists reveal whether statistical monitoring is genuine or decorative. If every recorded dimension sits exactly at nominal with zero variation across hundreds of parts, that's not a capable process—it's likely data filled in after the fact. Real charts show drift, occasional out-of-control points, and corresponding notes about what was done. Honest documentation of a process upset, followed by a verified correction, is far more valuable than a flawless spreadsheet that no one could believe came from actual production.
FAQ
You need to pin down denier per filament, breaking tenacity, elongation at break, and hot air shrinkage. These four form the backbone of performance. If a supplier hesitates to share exact values for each production lot rather than a generic datasheet, that hesitation itself is a red flag.
Ask for statistical process control data covering at least ten consecutive batches, not just one impressive certificate. Look at the coefficient of variation for tenacity. A trustworthy mill will show variation below three percent, while anything above five percent suggests unstable polymerization or poor spinning control.
Insist on testing according to ASTM D2256 or ISO 2062 with a gauge length that matches your actual stress conditions. Elongation dictates how the yarn absorbs sudden tension spikes during weaving. If the value is too low, you get brittle breaks at the loom; too high and the fabric loses dimensional stability.
Look for forced air oven aging tests run at temperatures that reflect real exposure, usually around 180 degrees Celsius for nylon 6. A serious lab will also track tenacity retention after aging and be willing to show you their raw data curves. If they only cite a single melting point number, they are not doing meaningful thermal work.
Finish level and uniformity can make or break warp knitting or weaving. Request a specific finish percentage by weight, along with a certificate showing even application across the package. Then ask for a trial cone from the exact finishing line they will use for production. A finish that is too low creates static and broken filaments, while too much leads to deposit buildup on guides.
Nylon 6 absorbs moisture from the air, and excess water acts as a plasticizer. That changes your measured tenacity and elongation, so you might approve a lot that performs differently once conditioned. Set a strict limit, typically below 4.5 percent by weight at standard atmosphere, and verify with a Karl Fischer titration rather than a simple oven dry method.
A serious supplier offers a lot traceability record that links raw polymer chips, spin line, draw ratio, finish application, and final package winding. The record should include the date range of production, operator shift, and any process adjustments. Without that chain of custody, you cannot isolate the cause of a sudden quality drop in your own plant.
Use accelerated weathering chambers that follow a recognized cycle, such as alternating UV exposure and condensation. Request comparative data between their yarn and a known reference sample under identical chamber conditions. Then look at retained breaking strength after a specified number of hours. A good supplier will define the exact lamp type, irradiance level, and temperature, not just say the yarn is UV stable.
Conclusion
A reliable high tenacity nylon 6 filament yarn supplier should be able to show you more than a polished data sheet. Ask for lot-level polymer batch traceability that links each finished spool back to its resin lot and production date. If a supplier cannot produce that chain of custody, you are left trusting promises instead of evidence. Tenacity claims deserve the same scrutiny: request an independent test protocol, not just a certificate generated in-house. The numbers that matter in the field often appear only after winding, so pay close attention to elongation and shrinkage specs that are measured under the same tension and temperature conditions your downstream process will use. Even small differences in these values can change how the yarn behaves on a braider, loom, or sewing line. Spooling and packaging deserve equal weight. Poor winding tension, dirty contact surfaces, or repurposed packaging can introduce contamination that is invisible at receiving inspection but shows up as breaks or weak points later.
Beyond the spec sheet, ask to read actual production logs from the runs that made your yarn. Look for run-to-run consistency signals such as stable extruder temperatures, consistent draw ratios, and low levels of filter pressure fluctuation. A supplier with genuine process control will have this data readily available and will not hesitate to walk you through it. Their documentation should reveal how they handle deviations, how often they recalibrate test equipment, and whether they re-qualify material after any process change. If the paperwork only contains final averages and no trace of raw measurements, treatment of outliers, or corrective actions, that is a warning sign. The strongest suppliers treat quality as a recorded, auditable sequence of decisions rather than a final stamp on a certificate.
Contact Us
Contact Person: CONNIE
Email: [email protected]
Tel/WhatsApp: 86-0512-53671634
Website: https://www.lida-yarn.com/